Recent innovations in large capacity refrigerated centrifuges technology focus on the improvement of automation as well as information integration. Intelligent models now communicate with laboratory information management systems so that the recording of experimental parameters is no longer problematic. Noise reduction modules and ergonomic covers have also increased user comfort and safety. Also, controlled temperature chambers and high-speed rotors facilitate the handling of sensitive material without degradation. Such technology renders large capacity refrigerated centrifuges equipment more adaptable to varying research needs, offering unparalled precision in particle separation and purification processes in countless industries.
The diversity of large capacity refrigerated centrifuges applications shows its diversity to modern technology. Aerospace engineers utilize it to check the material properties under intense centrifugal stress. Nanotechnology utilizes it to segregate particles at micro and nanolevel for analysis and manufacturing purposes. Hospitals rely on large capacity refrigerated centrifuges for testing, ensuring accurate plasma and serum analysis. Food processing industries utilize it to ensure product purity and uniformity. Additionally, educational laboratories employ large capacity refrigerated centrifuges in teaching and experimentation, whereby students learn fundamental physics, chemistry, and biology concepts through hands-on demonstration.

The large capacity refrigerated centrifuges of the future will be innovative, intelligent, and integrated. With the advent of smart manufacturing, large capacity refrigerated centrifuges systems will operate independently on predictive analytics. Programs with machine learning will interpret vibration patterns to optimize performance with minimal human involvement. Renewable energy integration will make operation more sustainable, and modular design will facilitate instant replacement of parts. Data visualization software will be more sophisticated, providing real-time feedback on the separation process. This blend of mechanical precision and intelligent technology will place large capacity refrigerated centrifuges at the forefront of international scientific advancement.

Proper maintenance and care of large capacity refrigerated centrifuges are essential for ensuring accuracy, safety, and long life. Regular checking of rotors for cracks and corrosion eliminates mechanical failure and imbalance. Users must clean the chamber with mild detergent and must not use abrasive chemicals that will damage surfaces. Regular calibration checks must be conducted to ensure speed accuracy. Greasing moving parts according to the manufacturer's recommendation increases motor life. Upon each use, samples need to be withdrawn at once, and open lids to prevent condensation. Periodic maintenance and records provide consistent operation.
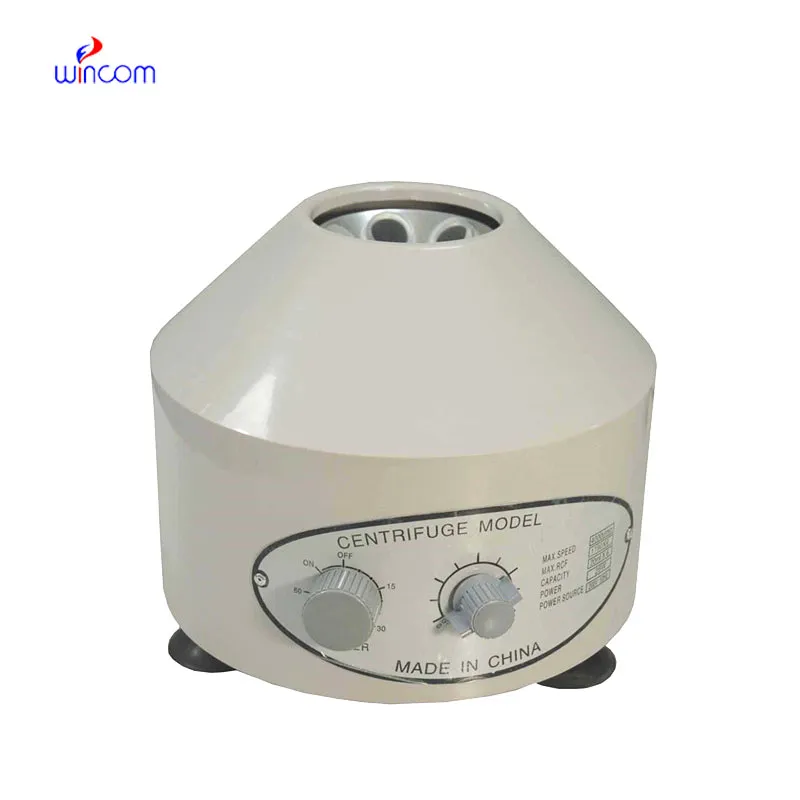
A large capacity refrigerated centrifuges is a universal gadget designed to separate parts in a mixture through sheer spinning power. A large capacity refrigerated centrifuges operates through the principle of sedimentation, in which heavier particles move outwards and lighter particles remain at the center. Employed within laboratories, clinics, and industry in general, a large capacity refrigerated centrifuges may be utilized to separate materials such as blood plasma, proteins, and chemical reagents with accuracy. Modern large capacity refrigerated centrifuges exist in various forms, from benchtop to industrial types and ultracentrifuges, all for specialized applications. They are accurate and reproducible, a necessity in production and research.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
We’ve used this centrifuge for several months now, and it has performed consistently well. The speed control and balance are excellent.
The microscope delivers incredibly sharp images and precise focusing. It’s perfect for both professional lab work and educational use.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Could you share the specifications and price for your hospital bed models? We’re looking for adjus...
We’re looking for a reliable centrifuge for clinical testing. Can you share the technical specific...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko