In modern-day lab environments, the large capacity refrigerated centrifuge wholesaler is not just a separation apparatus—it is precision engineering. With simple-to-view digital displays and microprocessor controls, it makes it easy for scientists to quickly adjust variables like acceleration and deceleration rates. Other models come equipped with onboard diagnostics that analyze rotor condition and operating performance. High-end safety features like automatic lid interlocks and imbalance detection offer protection at every cycle. With more rapid and consistent processing needed in industries, large capacity refrigerated centrifuge wholesaler technology keeps up with stability, precision, and greater throughput capability.
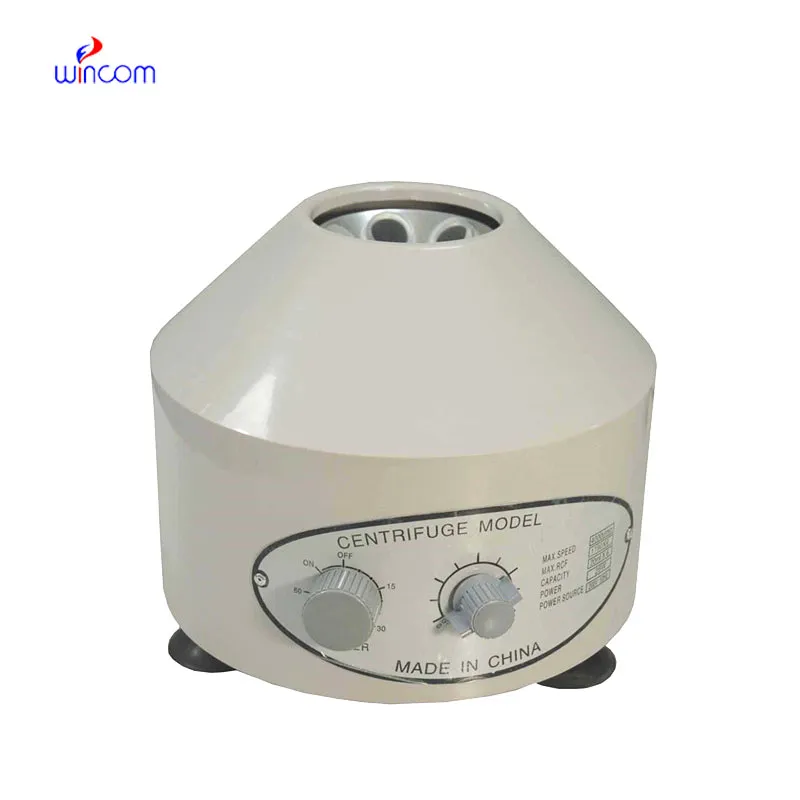
The versatility of large capacity refrigerated centrifuge wholesaler can be seen in its application to numerous specialized fields. In marine biology, it helps one analyze plankton and microbial samples. In food science, it helps with the accurate measurement of fat and protein content. The electronics sector employs large capacity refrigerated centrifuge wholesaler for purifying liquid crystals and conductive materials. In environmental protection, large capacity refrigerated centrifuge wholesaler facilitate tracking of pollutants and studies on recycling. They aid in veterinary medicine in blood diagnosis and disease investigation. With these uses, large capacity refrigerated centrifuge wholesaler bring about innovation through offering dependable means for analyzing as well as separating materials.

{Keywords} in the future will evolve into fully networked instruments in smart laboratories. They will "communicate" with other analytical instruments through built-in digital platforms, making experimental workflows easier. Equipped with self-diagnostic systems, maintenance needs will be identified before any issues arise. Future large capacity refrigerated centrifuge wholesaler models will emphasize energy efficiency and portability without compromising on speed or accuracy, while integration with robotics, AI-driven optimization, and user-friendly interfaces will redefine operations standards. In production and research environments, large capacity refrigerated centrifuge wholesaler will play a key role in achieving higher productivity and sustainable performance.

For optimal performance, large capacity refrigerated centrifuge wholesaler equipment needs to be handled cautiously and carefully. Operators need to ensure that rotors are balanced before use to avert vibration and wear. Regular cleaning of inner and outer surfaces prevents residues from building up that can impact results. Electric wiring should be inspected for loose or damaged cables. Storage of large capacity refrigerated centrifuge wholesaler in a clean, temperature-controlled environment keeps its components. Regular professional maintenance and replacement of worn parts on schedule ensure smooth and efficient use of the device over time.
A large capacity refrigerated centrifuge wholesaler makes the principle of rotational motion a tool of scientific inquiry and industrial productivity. Unrelenting spinning power applied to it fractions different materials in a sample on the basis of weight. It makes necessary procedures such as the analysis of blood, protein separation, and sewage treatment possible. large capacity refrigerated centrifuge wholesaler today combine strength with precision by offering variable speed ranges and advanced control mechanisms. Their use also extends beyond laboratories to fields like aerospace and environmental monitoring, showing both their scientific and utilitarian applications.
Q: How is a centrifuge different from a mixer or shaker? A: Unlike mixers or shakers that blend materials, a centrifuge separates components based on density through high-speed rotation. Q: What power requirements does a centrifuge need? A: Most benchtop centrifuges use standard AC power, while industrial units may require higher voltage for greater speed and capacity. Q: Can a centrifuge be used in pharmaceutical production? A: Yes, centrifuge equipment is widely used to purify chemical compounds and biological materials during drug manufacturing processes. Q: How do I prevent vibration during operation? A: Ensure all tubes are evenly loaded, rotors are clean, and the machine is placed on a stable, level surface. Q: What is the lifespan of a centrifuge? A: With regular maintenance and proper usage, a centrifuge can last for many years while maintaining consistent performance.
I’ve used several microscopes before, but this one stands out for its sturdy design and smooth magnification control.
We’ve used this centrifuge for several months now, and it has performed consistently well. The speed control and balance are excellent.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re currently sourcing an ultrasound scanner for hospital use. Please send product specification...
Hello, I’m interested in your water bath for laboratory applications. Can you confirm the temperat...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko